Choosing the best printed circuit board assembly partner in China takes more than comparing unit prices. A capable supplier should explain its process clearly, from component sourcing and solder paste inspection to reflow, testing, and final packaging. Ask how the team handles prototype changes, component substitutions, and production records. Details matter.
A factory’s equipment list is only a starting point. Request relevant certifications, sample inspection reports, and clear answers about traceability and defect handling. If your board uses fine-pitch components, check how the supplier verifies solder joints and tests assembled boards. A low quote may exclude tooling, testing, or shipping. Read the terms carefully.
No supplier is perfect. The useful question is how quickly it identifies problems and documents corrective action. A polished presentation is not proof. Ask for evidence. This guide compares practical factors that buyers can assess before choosing a partner, including engineering support, quality controls, communication, lead times, and cost transparency. It also considers the trade-offs between a quick prototype run and stable volume production. Your priorities may differ: a startup validating a compact sensor board needs different support from a manufacturer ordering thousands of control boards. Clear requirements make comparisons more reliable, and direct technical questions can reveal gaps early. The right choice is not simply the largest factory or the cheapest quote. It is a supplier whose documented capabilities match your design, schedule, and quality expectations.
Best Printed Circuit Board Assembly in China?
What Printed Circuit Board Assembly Includes
Printed circuit board assembly, or PCBA, turns a bare board into a working electronic unit. It includes checking design files, sourcing components, applying solder paste, placing parts, soldering, and testing. In surface-mount assembly, machines position tiny resistors and chips onto paste-coated pads before the board passes through a reflow oven. Through-hole parts, such as connectors, are inserted into drilled holes and soldered. Small parts matter. A misplaced component or weak solder joint can stop the whole unit from working.
Assembly also involves inspection and verification. Automated optical inspection checks component position and solder appearance; electrical tests can confirm continuity and detect shorts. Depending on the product, the process may include programming and functional testing in a fixture. The World Semiconductor Trade Statistics organization reported global semiconductor sales of $526.8 billion in 2023. That figure is not an assembly-quality measure, but it shows the scale of the component supply chain behind each board. Traceability for parts and process settings therefore deserves attention. The boundary can blur: a supplier may assemble boards, source components, or offer both. Buyers should check which steps are included, what test records are provided, and how defects are handled. A polished inspection report helps, but it cannot replace clear acceptance criteria agreed before production.
A typical PCBA workflow combines board and component preparation, soldering, inspection, and testing. The sequence can vary by design and production requirements.
Bars indicate workflow order only (1 = first); they do not represent time, cost, or quality. SPI, AOI, X-ray, and functional testing are used as appropriate to the assembly.
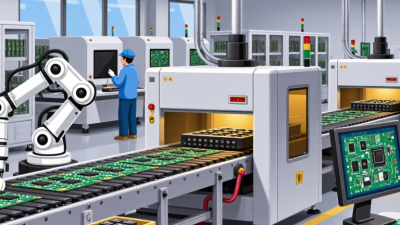
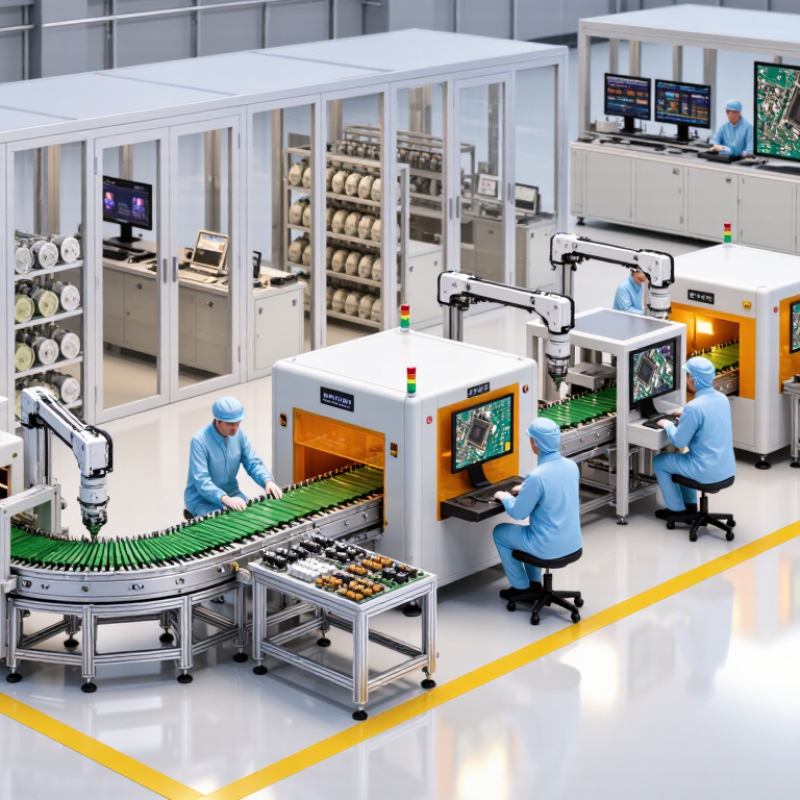
PCB assembly in China usually starts with engineering review, not the placement line. Engineers check component footprints, panel layout, solder-mask clearances, and whether parts are available. A stencil then deposits solder paste onto the board. Pick-and-place machines position tiny components, sometimes at high speed. Reflow ovens melt the paste through controlled temperature zones. Small details matter. Moisture-sensitive packages need careful handling, and a poor thermal profile can weaken solder joints.
After reflow, automated optical inspection checks component position and visible solder defects. X-ray inspection may be used for hidden connections under BGA packages. Through-hole parts are soldered separately, followed by electrical testing and, where specified, functional checks. Prismark’s 2023 PCB industry assessment estimated worldwide PCB production value at about US$68.9 billion. That figure describes bare-board production, not assembly revenue, so it should not be treated as a direct measure of China’s PCBA output. Still, it shows the scale of the supply chain supporting assembly. The process is rarely as tidy as a diagram suggests: a substitute component or a small design change can require fresh validation. A fast line is not automatically a stable one.
Best Printed Circuit Board Assembly in China?
Key Standards for Evaluating Assembly Quality
A capable assembly partner should show how its quality controls match the board’s intended use. IPC-A-610 provides criteria for judging electronic assemblies, while J-STD-001 addresses soldered connections. The required class and acceptance limits should be agreed before production, not guessed during inspection. Details matter. A bright, clean board can still hide a weak joint beneath a component.
Ask how incoming materials, solder paste, and process settings are controlled. For surface-mount assembly, documented reflow profiles help confirm that components receive suitable heat. Automated optical inspection can catch misplaced parts, polarity errors, and visible solder defects. It cannot see every hidden joint. X-ray inspection may help assess certain bottom-terminated components, but results still need trained interpretation.
Traceability should connect a finished board to relevant material batches, production records, and inspection results. Request sample reports, defect data, and the corrective actions taken after failures. Then check whether those records match the actual board revision and order. This step is easy to rush. It should not be. No single certificate proves consistent workmanship, and even a strong process can miss defects; a practical evaluation combines standards, evidence, and clear communication.
Use these standards and measurable checks to compare PCB assembly suppliers. Acceptance requirements depend on the product, assembly class, contract, and applicable standard revision.
| Evaluation Dimension | Relevant Standard or Benchmark | What to Verify | Practical Evaluation Guidance |
|---|---|---|---|
| Soldering workmanship | IPC J-STD-001; IPC-A-610 | Documented soldering requirements and inspection criteria for the agreed product class, including joints, leads, and component placement. | Request the supplier’s inspection criteria and sample inspection records. Agree on the applicable class and revision in the purchase documents; acceptance limits vary by class and product. |
| Product acceptance class | IPC-A-610 Classes 1, 2, and 3 | Whether the specified acceptance class matches the product’s intended use and reliability needs. | Class 1 generally covers general electronic products, Class 2 dedicated-service products, and Class 3 high-performance or harsh-environment products. The class should be explicitly agreed rather than assumed. |
| Rework and repair control | IPC-7711/7721 | Controlled procedures for component removal, replacement, repair, and modification, with records for reworked assemblies. | Check that rework is authorized, performed using documented methods, and followed by suitable inspection and testing. Define rework limits for sensitive components and pads. |
| Process quality management | ISO 9001:2015 | A quality management system covering document control, corrective action, supplier control, process monitoring, and continual improvement. | Verify certificate scope, issuing body, validity, and whether the certified site and activities cover the assembly work being quoted. |
| Medical-device quality system, when applicable | ISO 13485:2016 | Quality management controls relevant to organizations supplying products or services for medical devices. | For medical projects, confirm that the certificate scope and documented controls fit the specific supply-chain role and customer requirements. |
| Automotive quality system, when applicable | IATF 16949:2016 | Automotive-sector quality management requirements, including applicable customer-specific requirements. | For automotive programs, verify certification scope and site, and confirm that the supplier can meet the program’s traceability, change-control, and quality-planning requirements. |
| ESD protection | ANSI/ESD S20.20 or IEC 61340-5-1 | An electrostatic-discharge control program for relevant handling, assembly, storage, and packaging operations. | Ask for the ESD control plan, training and audit records, and evidence that grounding and workstation checks are performed at defined intervals. |
| Material compliance | RoHS Directive 2011/65/EU, as amended; REACH Regulation (EC) No 1907/2006 | Material declarations and supporting evidence for applicable substance restrictions and customer requirements. | Specify the required market and compliance scope. Request current declarations and supporting records for the relevant bill of materials; do not treat a general statement as product-specific evidence. |
| Inspection and test coverage | Contract-defined control plan and test specification | Appropriate inspection and electrical testing, such as automated optical inspection, X-ray inspection for applicable hidden joints, and in-circuit or functional testing where designed. | Review the test plan, defect criteria, equipment calibration records, and sample reports. Test coverage should be defined for the board design and risk; no single test method verifies every defect type. |
| Process consistency and yield | Customer-agreed key performance indicators | First-pass yield, defect trends, corrective actions, and evidence of process monitoring. | Set targets in the contract or quality plan rather than treating a generic yield figure as a universal standard. Review results by product and production period, including how failures and rework are counted. |
| Traceability and change control | Customer-specific requirements and applicable quality-system procedures | Ability to link assemblies to relevant production lots, materials, inspection/test records, and approved engineering revisions. | Define the required traceability level before production. Check sample records and confirm that component substitutions, process changes, and revision updates require documented approval where applicable. |
| Delivery and packaging condition | Purchase order, packaging specification, and handling requirements | Protection against electrostatic discharge, moisture, contamination, and physical damage during storage and transport, as applicable to the components and product. | Confirm packaging instructions, moisture-sensitive-device handling where relevant, labeling, and shipment inspection records against the agreed product and logistics requirements. |
Note: Standards and certification do not by themselves guarantee product quality. Confirm the applicable revisions, product class, acceptance criteria, test plan, and evidence requirements in the contract or quality agreement.
Choosing a PCB assembly provider in China takes more than comparing unit prices. Look for engineers who review Gerber files, stack-up details, and bill-of-materials risks before quoting. A useful review may flag an oversized thermal pad or a hard-to-source connector. Small details matter. Ask how changes are recorded and whether the same revision reaches purchasing, production, and inspection.
Process control distinguishes dependable providers. Request evidence of solder-paste inspection, automated optical inspection, and X-ray checks for hidden joints when the package design requires them. For prototypes, ask how the line handles setup verification and first-article approval. For volume builds, examine defect trends, rework records, and lot traceability. Certifications can help, but a certificate alone cannot show how a specific board was built.
Communication is part of quality. Confirm who answers engineering questions, how quickly deviations are escalated, and whether delivery estimates account for component shortages and test time. Ask to see a sample inspection report or a redacted production traveler. Beware vague promises. A provider may have strong equipment yet weak feedback loops; that gap can leave a minor footprint or polarity issue unnoticed until assembly. No supplier is flawless. Check the evidence, not just the sales language, and consider which trade-offs your design can tolerate.
A capable partner should prove process control, not just quote a low unit price. Ask for a pilot build using your actual bill of materials, soldering requirements, and board finish. Review first-article records, AOI images, X-ray results for hidden joints, and test logs. Check that component lots can be traced from receiving inspection to finished boards. IPC-A-610 and J-STD-001 provide useful workmanship and soldering references; agree on applicable classes and acceptance criteria before production. Small details matter. A missing revision mark can cause a costly mix-up.
Assess delivery claims against external logistics data, but do not treat national rankings as supplier guarantees. The World Bank’s 2023 Logistics Performance Index placed China 19th among 139 economies. That offers context, not a forecast for your shipment. The WTO reported that global merchandise trade volume fell 1.2% in 2023, underscoring why schedules need realistic buffers. Request recent on-time delivery figures, separated by prototype and production orders, and ask how delays are communicated. Visit the facility when feasible; follow one job from incoming inspection to packing. If a remote audit is necessary, request dated process records and a live video walkthrough. I would still verify a sample independently. That step adds cost, but it can expose assumptions hidden by polished presentations.