Blog

How to Choose the Best Side Spray Retort in 2026?

Choosing the best Sides Spray Retort in 2026 is not just a capacity decision. The right system must heat every package consistently, fit the product and container, and support reliable production. Small details matter: basket spacing, spray nozzle placement, and how quickly operators can load a batch. A machine that looks efficient on a brochure may perform differently on a crowded production floor.

Market growth gives useful context, but it does not select the equipment for you. Grand View Research estimated the global retort packaging market at USD 4.1 billion in 2022 and forecast a 4.8% compound annual growth rate from 2023 to 2030. This figure covers packaging, not retort machinery, so it should not be treated as a direct measure of equipment demand. Still, it signals continued interest in shelf-stable packaged foods. The report is a starting point, not a buying specification.

For a practical comparison, assess container type, batch size, temperature uniformity, water use, controls, and service support. Ask suppliers for heat-distribution and heat-penetration evidence using your actual package and product. Then review cleaning access, spare-parts availability, and operator training. That sounds simple. It is not. A wider capacity range can help, but it may also raise energy use or complicate changeovers. There is no universal winner. This guide explains how to weigh the trade-offs and choose a Sides Spray Retort that matches your process, not merely the highest advertised output.
How to Choose the Best Side Spray Retort in 2026?

Understanding Side Spray Retorts and Their Operating Principles

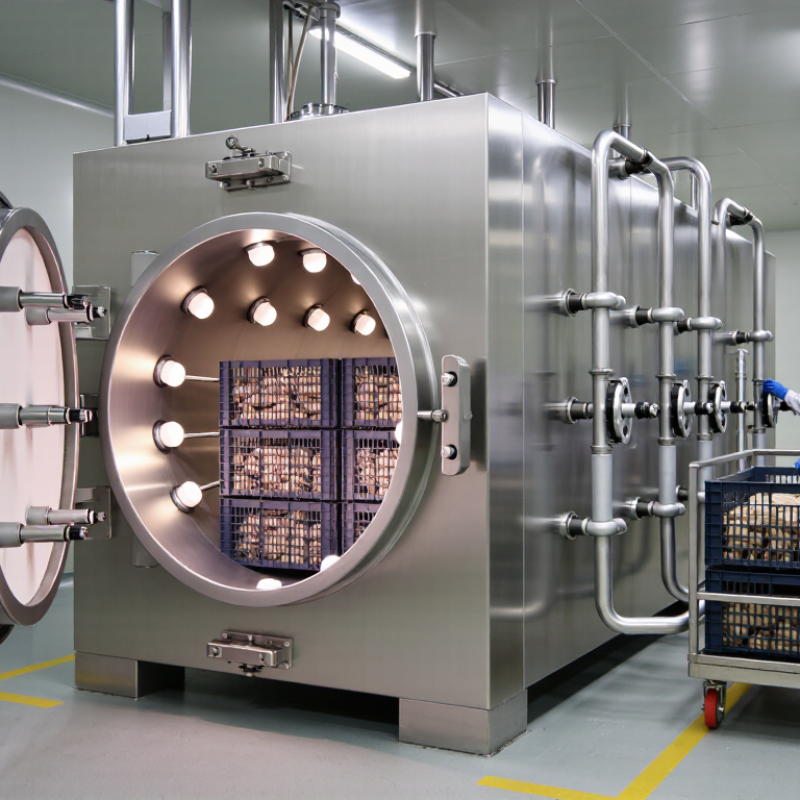
A side spray retort heats sealed food packages by circulating hot water through nozzles along the vessel walls. A pump keeps the water moving, helping it reach packages across the load. Unlike direct steam heating, this method uses water as the heat-transfer medium. The details matter. Basket spacing, package shape, and spray coverage can all affect heating.

Operators load the baskets, close the vessel, and bring the water to the required temperature. Air removal and controlled pressure help create stable conditions. The programmed holding period should begin only when the validated process conditions are met, not simply when a display reaches its target. Temperature sensors and routine checks help confirm that the load receives consistent treatment. Small detail, big effect.

During cooling, pressure may need to remain controlled to protect pouches, trays, or other sealed containers from distortion. A side spray system is not automatically suitable for every product or package. Heat penetration varies with food thickness, fill weight, and how containers are arranged. Even a tidy-looking load can hide uneven circulation. That part deserves scrutiny. Before choosing equipment, compare its controls, spray distribution, loading method, and ability to record process data with your actual production needs.

Matching Retort Capacity to Product and Packaging Requirements

When sizing a side spray retort, start with the actual package, not the largest vessel in a catalogue. Record container diameter, height, material, fill weight, and closure type. A pouch, glass jar, and metal can behave differently during heating and pressurization. Changes in product thickness or headspace can also affect heat transfer. That gap matters.

Estimate capacity from usable basket space and a loading pattern operators can repeat. A retort may hold many containers on paper, yet tightly packed baskets can restrict spray circulation. Check spacing between packages, basket layers, and spray nozzles. Compare the practical load with daily production, batch changeovers, and cleaning time. Bigger is not always better. An oversized chamber may run partly empty; a tight fit can make loading awkward.

Request a trial using representative product and packaging, with temperature sensors in likely slow-heating locations. Review heating time, temperature distribution, cooling needs, and batch records with a qualified process specialist. Confirm capacity against the validated process, not chamber volume alone. It is tempting to compare only containers per cycle, but that number misses important details. Recheck the assumptions whenever package size or recipe changes. Small details count.

Comparing Spray Systems, Temperature Control, and Process Performance

Choosing a side spray retort means comparing how evenly each system distributes heat, not just how many nozzles it has. Spray patterns, water flow, and load spacing all matter. A tightly packed basket can block circulation, leaving some packages slower to heat. Ask for temperature-mapping results using a load similar to your own. A clean spray pattern is useful. Real loads are messier.

Temperature control deserves equal attention. Look for calibrated sensors, stable control during come-up and holding, and clear records for each cycle. Small fluctuations may affect process consistency, especially with dense products or different package sizes. The setpoint alone is not proof of uniform heating. Independent validation should identify the slowest-heating location and confirm the required process there. Details matter.

Process performance also includes cooling and repeatability. Compare cycle times, water use, pressure stability, and how quickly the system returns to target conditions between loads. Ask how operators detect blocked nozzles and verify sensor accuracy. These checks can reveal practical weaknesses before installation. There is no universal winner. A faster cycle may not suit every product, and supplier data may not match your basket, package, or filling variation. I would treat any perfect-looking chart cautiously and request a representative trial.

Checking Safety Standards, Automation, and Maintenance Needs

When choosing a side spray retort, treat safety controls as part of the process, not optional extras. Check that vessel documentation, pressure protection, door interlocks, and temperature sensors match the intended operating range. For U.S. low-acid canned foods, FDA rules in 21 CFR Part 113 require scheduled processes and processing records. Confirm that the retort’s controls can capture the data your qualified process authority needs. Small details matter. A sensor that is hard to remove can become a calibration problem.

Automation should make process records clearer, not hide them behind complex screens. Deloitte and MAPI’s 2024 Smart Manufacturing survey found that 92% of manufacturers view smart manufacturing as a driver of competitiveness in the next three years. That is a broad manufacturing finding, not a retort performance guarantee. Ask for a live demonstration of recipe control, alarms, batch reports, and safe recovery after a power interruption. Then test the workflow with the operators who will use it.

Maintenance access deserves equal attention. Inspect spray nozzles, pumps, seals, strainers, and drain points on the actual machine. Can a technician reach them without removing major panels? Ask for recommended inspection intervals, spare-part lead times, and service documentation. A polished interface is useful, but it cannot compensate for clogged nozzles or poor records. I would still question any supplier estimate that assumes every cleaning and changeover runs perfectly. In real plants, it rarely does.

Evaluating Total Cost and Selecting a Reliable Manufacturer

A side spray retort should be judged by its running cost, not just its purchase price. A low quotation can hide higher water, steam, electricity, or labor use. Ask for utility estimates at your expected batch size, along with cycle time and loading capacity. Small differences matter. Extra minutes per cycle can reduce daily output.

Build a five-to-ten-year estimate that includes installation, operator training, routine inspections, replacement seals and spray nozzles, calibration, and downtime. Request a clear maintenance schedule and prices for common spare parts. Check whether cleaning and service access fit your plant layout. A cheap component is not cheap if replacement takes weeks.

Assess the manufacturer through evidence, not promises. Ask for references from plants with similar products and operating volumes. Review sample test records, equipment documentation, and the proposed acceptance test. Confirm who handles commissioning, troubleshooting, and spare-part requests, and how quickly they respond. A polished brochure is weak evidence. Leave room for uncertainty, too: actual utility use may differ from estimates, so ask what assumptions shaped the quotation. A site visit can reveal details that a spreadsheet misses.

How to Choose the Best Side Spray Retort in 2026? - Evaluating Total Cost and Selecting a Reliable Manufacturer

Evaluation Dimension What to Assess Evidence or Data to Request Total-Cost Impact
Process and product fit Confirm that a water-spray process suits the product, container material, closure, and required thermal process. Side-spray systems circulate heated water through spray nozzles; performance depends on the retort design and load arrangement. A written compatibility review covering product type, container dimensions, package orientation, loading pattern, and the proposed process conditions. Mismatch can lead to rework, package damage, lower throughput, or costly equipment changes.
Temperature distribution Check that the spray system distributes water consistently throughout the loaded vessel. Nozzle layout, flow, load spacing, and water circulation all affect heat distribution. Temperature-distribution test results using representative baskets and the intended production load; ask how test locations and acceptance criteria are defined. Uneven distribution may constrain loading or cycle time and can require additional testing or corrective work.
Thermal-process validation The scheduled process must be established for the specific product and package by qualified process authorities. Equipment cycle settings alone do not establish product safety or commercial sterility. Support for heat-penetration studies, process-authority review, instrument calibration, and documented changes to the approved process. Validation, documentation, and later requalification require time and specialist resources; clarify which services are included in the quotation.
Capacity and throughput Evaluate usable vessel volume, baskets per cycle, loading and unloading time, cycle duration, and expected operating schedule—not just nominal vessel dimensions. A proposed cycle and capacity calculation based on the actual container, basket configuration, load pattern, and planned production hours. Insufficient usable capacity can increase labor and the number of cycles needed; oversizing can raise purchase and utility costs.
Utilities and operating cost Compare steam, electricity, cooling water, and process-water requirements across the complete cycle, including heating, holding, cooling, and standby conditions. Utility consumption estimates per cycle, stated assumptions, connection requirements, and any options for heat recovery or water reuse. Utility consumption can be a significant recurring cost. Actual cost depends on local tariffs, cycle recipe, load, and operating hours.
Water management and sanitation Review water circulation, drainage, filtration, cleanability, and measures to limit deposits or nozzle blockage. Confirm the materials and finishes suit the plant’s process-water conditions. Water-quality requirements, cleaning instructions, drain details, filtration specifications, and a list of routine inspection points. Water treatment, cleaning labor, and scale or corrosion control add to lifecycle costs if not addressed in the design.
Controls and records Check recipe control, alarms, sensor monitoring, data retention, access permissions, and the ability to review cycle records. Confirm which functions are standard and which are optional. Controls specification, sample cycle report, backup and export method, calibration procedures, and a demonstration of alarm handling. Optional software, integration, training, and record-storage requirements can increase installation and ongoing support costs.
Maintenance and spare parts Assess access to pumps, valves, seals, sensors, nozzles, and other wear parts. Ask how routine service can be performed and what maintenance tasks require specialist support. Recommended preventive-maintenance schedule, spare-parts list, expected parts availability, and service response terms for the installation region. Labor, spare parts, and unplanned downtime should be included in lifecycle comparisons, not treated as incidental costs.
Installation and integration Determine site requirements for foundations, access, utilities, drainage, ventilation, loading equipment, and connection to existing production systems. A site-preparation checklist, installation scope, interface drawings, commissioning plan, and clear responsibility split between purchaser and supplier. Building work, utility upgrades, freight, commissioning, and production interruption can materially change the installed cost.
Manufacturer reliability Evaluate relevant retort experience, engineering documentation, quality controls, commissioning capability, training, and after-sales service coverage. References for comparable applications, documented inspection and test procedures, warranty terms, service contacts, and examples of manuals and as-built documents. A lower purchase price may be offset by weak documentation, delayed support, difficult maintenance, or extended downtime.
Total cost of ownership Compare the full expected cost over the same evaluation period: equipment, installation, utilities, labor, maintenance, validation, training, and downtime. A like-for-like quotation with inclusions, exclusions, assumptions, warranty coverage, payment terms, and a separately stated estimate for recurring costs. No single quoted price represents total ownership cost. Compare suppliers using the same load, operating hours, utility rates, and scope assumptions.

Note: Equipment performance, utility consumption, cycle time, and lifecycle cost are application-specific. Confirm figures through a documented proposal, site review, and testing with the intended product and package.